Mining wire ropes
Bulker Industrial Mining Wire Ropes are engineered to conquer the earth’s harshest subterranean and open-pit environments. When equipment downtime costs thousands per minute, Bulker Wire Ropes deliver unstoppable reliability for draglines, shovel hoists, and deep-shaft mine winders.
Built to outlast: the ultimate mining triple shield
Crack resistance
Forged from ultra-pure, high-ductility steel alloys and precision-wound to disperse extreme cyclic bending stress. Our ropes absorb sudden shock loads without developing micro-fractures or structural fatigue.
Corrosion immunity
Infused with our signature BulkerGal-A3 zinc-aluminum molecular armor and pressure-injected with hydro-repellent synthetic lubricants. This dual barrier completely blocks acidic mine water, sulfur, and deep-earth moisture from rotting the core.
Abrasion defiance
Engineered with high-density, outer-strand profiles and optional compacted wire layouts. This creates a smooth, ultra-hard exterior surface that minimizes friction against sheaves and relentlessly resists abrasive rock dust and grit.
Overview
Heavy-duty rigging & hoisting for mining
Premium heavy-duty rigging & hoisting solutions for global mining operations.
In the unforgiving environments of modern mining, operational continuity, extreme load resilience, and absolute safety are non-negotiable. BULKER WIRE ROPES engineered extraction solutions are uniquely qualified to withstand high cyclic bending stresses, abrasive dust, corrosive mine waters, and immense shock loads. Every millimeter of our rope is certified under our proprietary three-digit tracking protocol, BRM 391, ensuring guaranteed performance from the deep underground shaft to the point of global maritime export at the quay.
Comprehensive sector architecture
Our engineered wire solutions are tailor-made for specific operational conditions across all primary mining frameworks:
Open-pit mining
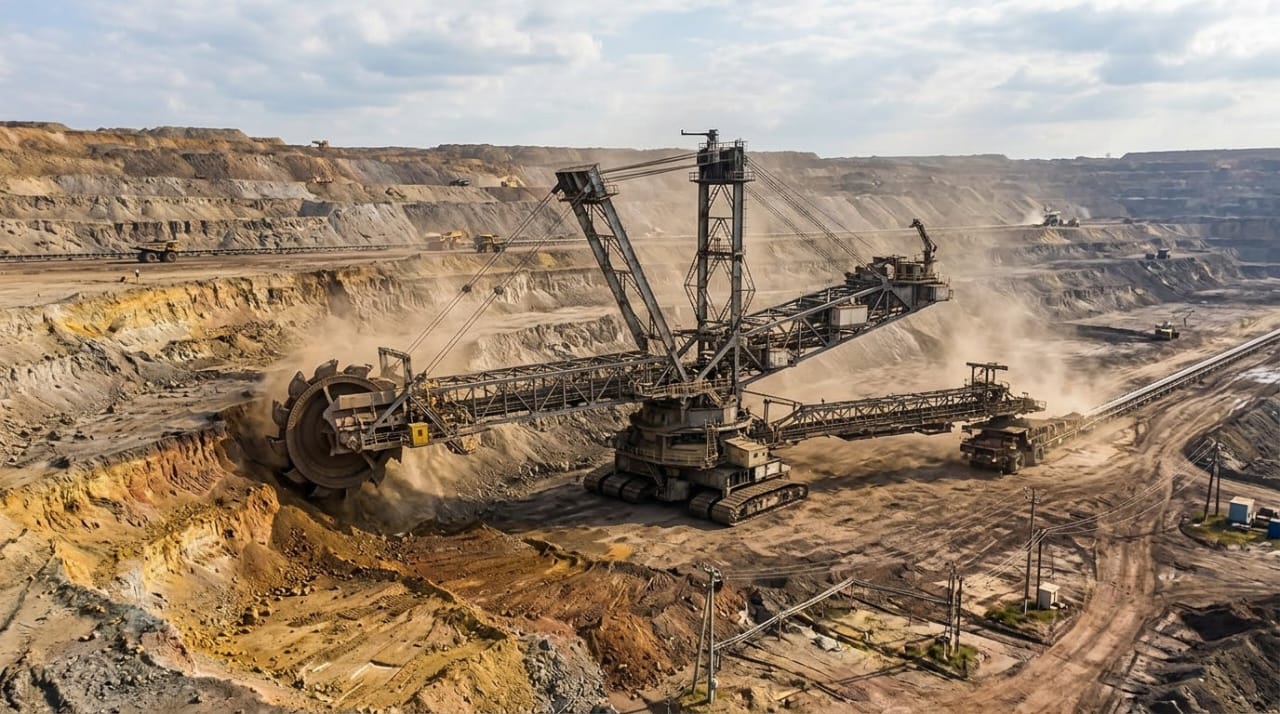
Resisting extreme weather variations, abrasive grit, shock vibrations, and heavy bending stress across massive surface operations.
Underground mining
Providing critical failure-preventative tensile strength and exceptional fatigue life for high-speed, high-depth vertical hoisting and shaft systems.
In-situ recovery & solution mining
Withstanding sustained immersion in chemically active liquids and corrosive chemical extraction setups.
Placer & marine mining
Countering continuous moisture, severe grit abrasion, and brackish underwater dredging environments.
Exhaustive equipment coverage
BULKER WIRE ROPES supplies high-performance configurations for every piece of machinery requiring wire ropes throughout the entire extraction, processing, and port handling lifecycle:
Surface excavation machinery
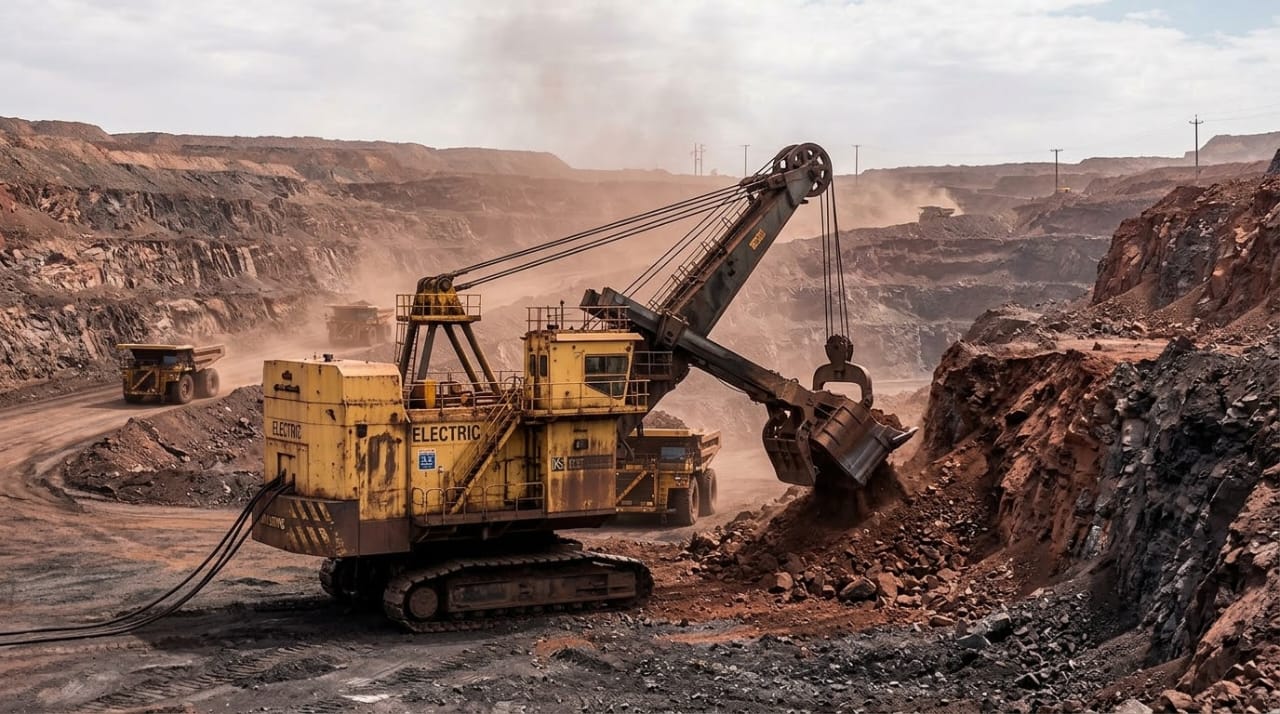
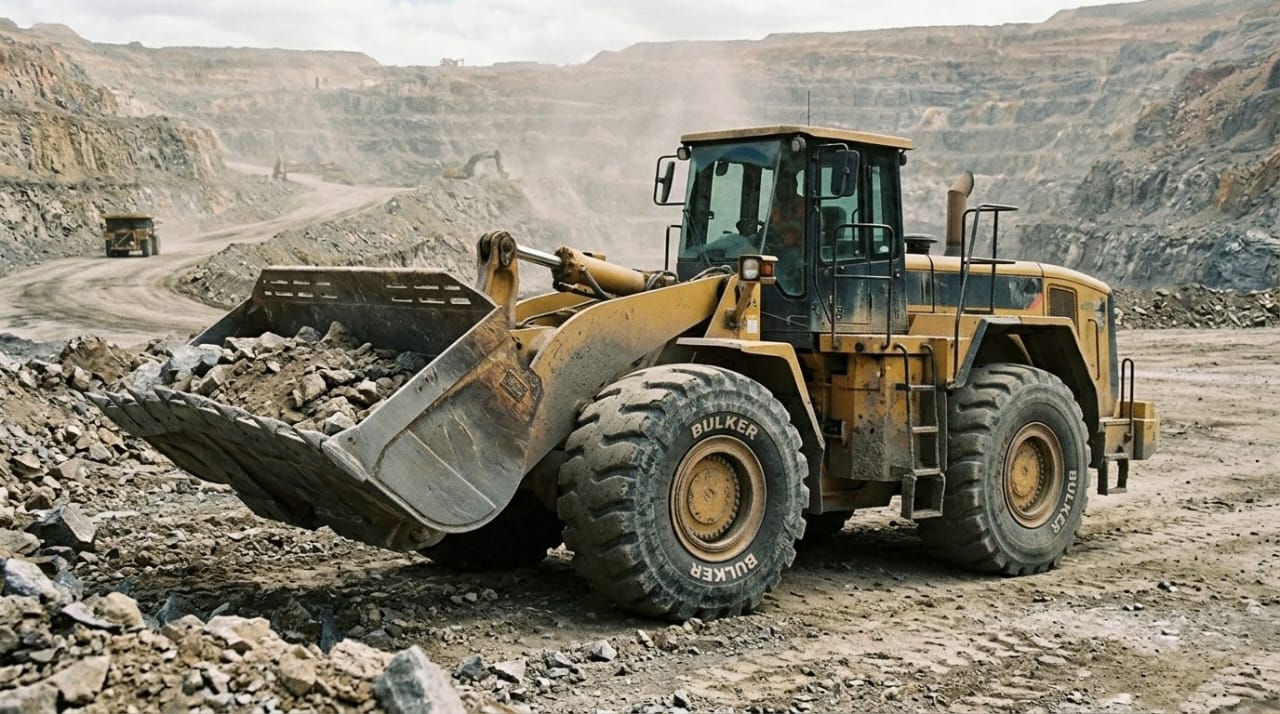
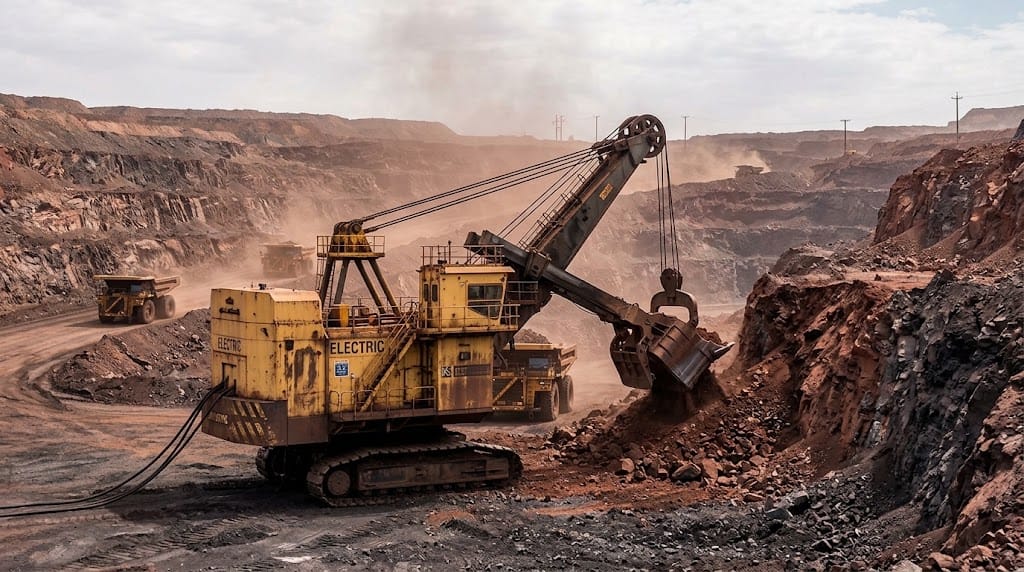
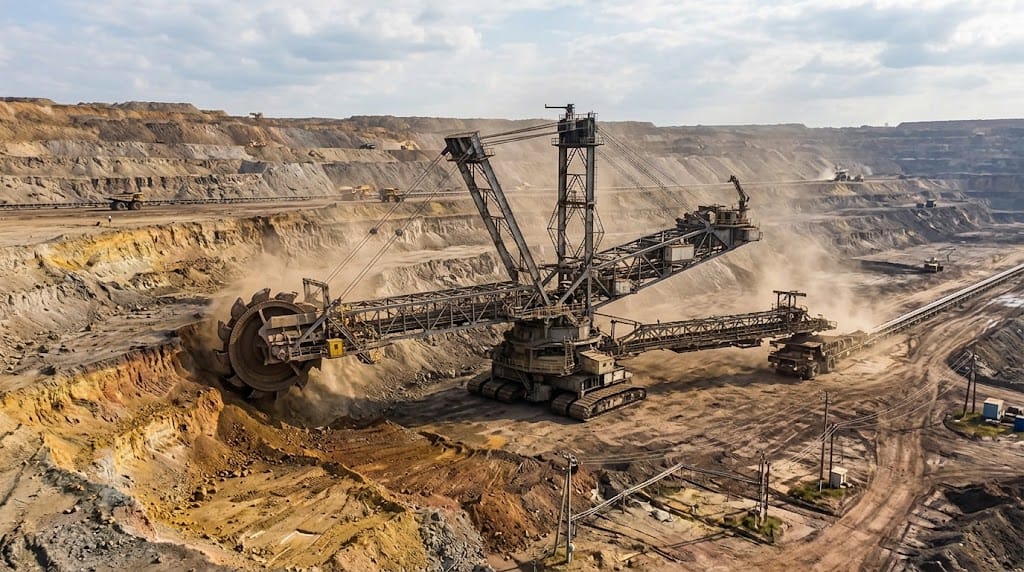
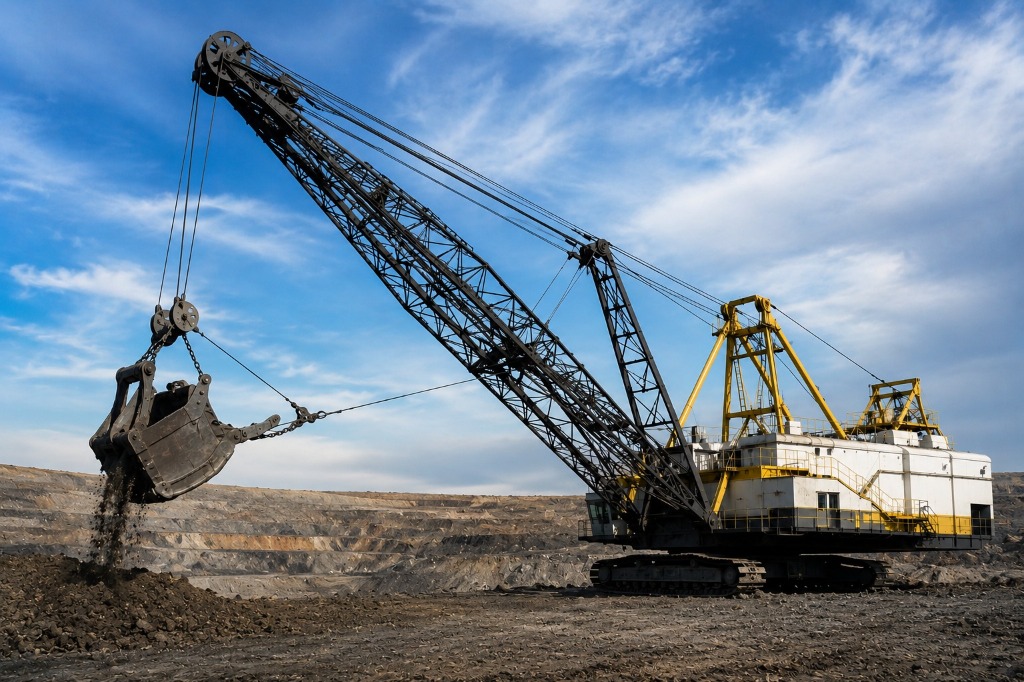
Electric Rope Shovels (Hoist, Crowd, Retract, and Dipper Trip ropes), Draglines (Hoist, Drag, Dump, and Boom Suspension ropes), Bucket Wheel Excavators, and High-Capacity Mobile/Crawler Cranes.
Underground infrastructure
Koepe/Friction Hoists, Drum Hoists (Single and Double Drum installations), Tail/Balance Ropes, Guide Ropes, Shaft Sinking Winches, Slushers, Scrapers, and Stage Winches.
Processing & heavy material logistics
Conveyor Tensioning Systems, Wagon Lifting Cranes & Tipplers (Heavy-duty high-diameter ropes specifically engineered for flipping and lifting bauxite wagons to dump raw ore for crushing/refinement).
Quay & port operations
Ship-to-Shore (STS) Quay Cranes, Stacker-Reclaimers, Ship Loaders, Continuous Vessel Unloaders, and Heavy-Duty Harbor Boom Hoists used at the quay for global mineral export.
The BULKER technical advantage
01 BRM 391 quality architecture
Our strictly enforced BRM 391 three-digit compliance framework certifies that every batch of wire ropes undergoes non-destructive electromagnetic testing, rigorous breaking load validations, and multi-stage grain boundary analysis. This ensures absolute traceability and a near-zero failure metric across maximum load ceilings.
02 Advanced corrosion & abrasion resistant coating
BULKER wire ropes are coated with a specialized zinc-aluminum-magnesium micro-alloy thermal shield integrated with a high-viscosity synthetic polymer core lubricant. This dual-action layer seals the inner strands against acidic mine runoff, high-salinity air at the quay, and heavy physical abrasion from flying ore particles—extending standard rope service life by up to 300%.
03 Rapid deliveries & global logistics hubs
We eliminate costly site downtime through an active network of strategically positioned distribution hubs. BULKER guarantees rapid delivery, custom spooling, and on-site engineering support directly to your remote mine site or export facility, dramatically reducing lead times from weeks to days.
Mining sector technical specifications table
The following matrix represents standard engineering specifications for premium BULKER WIRE ROPES utilized across mining and quay infrastructures, including our new specialized large-diameter bauxite wagon lifting rope classes:
| Application / equipment type | Nominal diameter | Rope construction class | Minimum breaking load | Specialized outer coating/lubrication |
|---|---|---|---|---|
| Electric rope shovel (hoist) | 52 – 64 mm | 8x37 IWRC compacted | 2,150 – 3,240 kN | Abrasion Poly-Shield / BRM 391 |
| Dragline (drag ropes) | 76 – 102 mm | 6x41 Filler Wire IWRC | 4,480 – 7,850 kN | Extreme Grip anti-wear compound |
| Underground Koepe friction hoist | 40 – 54 mm | Full Locked Coil | 1,850 – 3,400 kN | Galvanized anti-corrosive fluid |
| Underground drum hoist | 32 – 48 mm | 6x36 Warrington-Seale | 840 – 1,910 kN | Heavy duty core fill / BRM 391 |
| Shaft sinking / stage winch | 24 – 38 mm | 18x7 non-rotating class | 410 – 1,020 kN | Zinc-alum galvanized coating |
| Slushers & scrapers | 16 – 22 mm | 6x19 Seale fiber core | 145 – 280 kN | High friction synthetic grease |
| Conveyor tensioning system | 20 – 28 mm | 6x25 Filler Wire IWRC | 290 – 560 kN | Moisture block micro-lubricant |
| Wagon lifting (bauxite dump processing) – new | 68 – 82 mm | 8x49 premium compacted IWRC | 3,850 – 5,600 kN | Ultra-thick wear-resistant polish |
| Wagon lifting (bauxite dump processing) – new | 84 – 96 mm | 9x49 super-compacted IWRC | 5,820 – 7,540 kN | Dual-shield abrasion resistant armor |
Technical brochure
Surface mining
Engineered for extreme abrasion, high impact and harsh atmospheric exposure in open-pit operations.
Wire ropes for electric rope shovels, draglines, rotary blast-hole drilling rigs and haul-road recovery, from 38 to 111 mm.
6x19 · 6x36
Rope shovels, draglines & mine hoists
Engineered for extreme depths
Constructed to withstand harsh abrasive environments and the extreme tension of deep shaft operation. High-carbon steel composition and specialized lubrication for resistance to crushing and fatigue. Available in constructions such as the 6x19 and 6x36 classifications, designed for hoist, dragline and shovel applications.
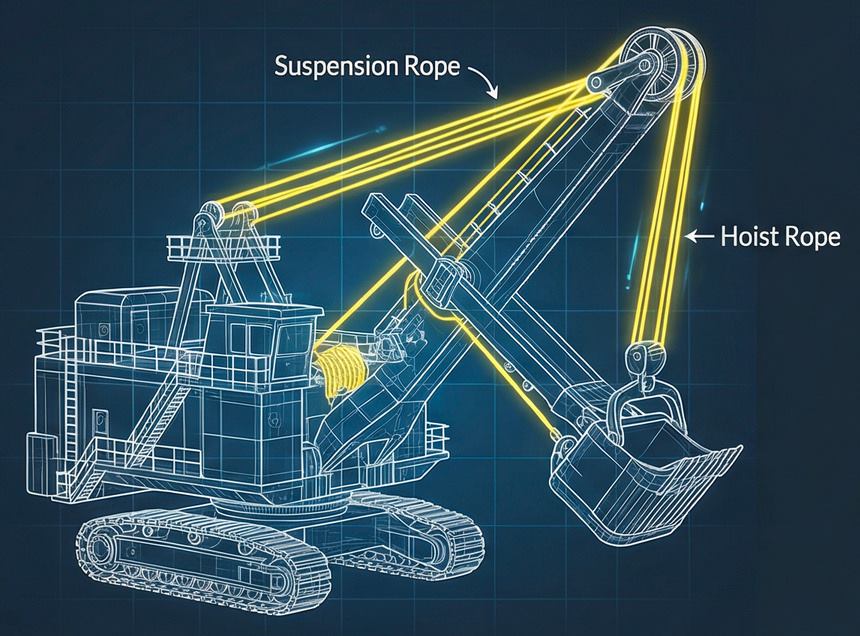
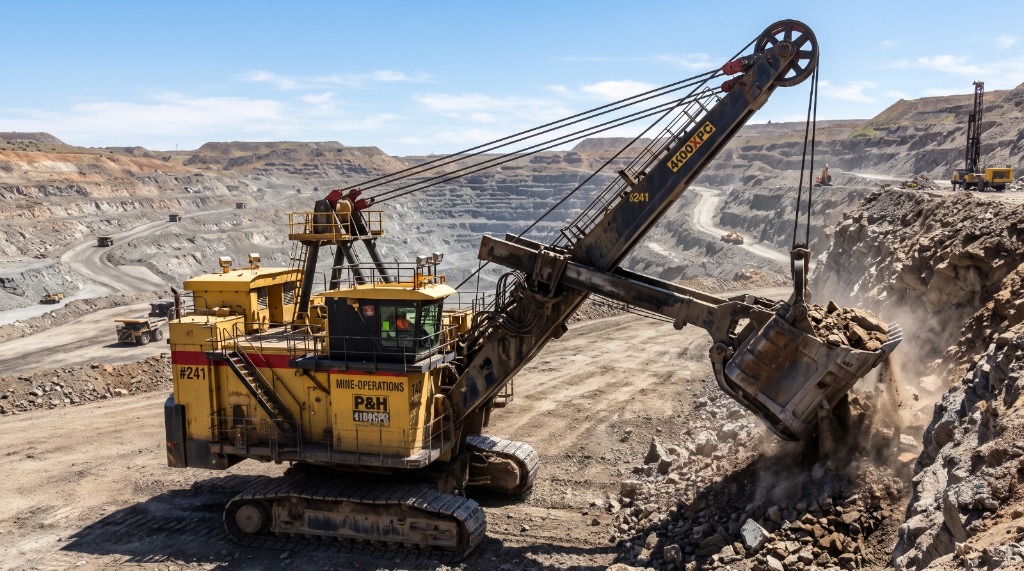
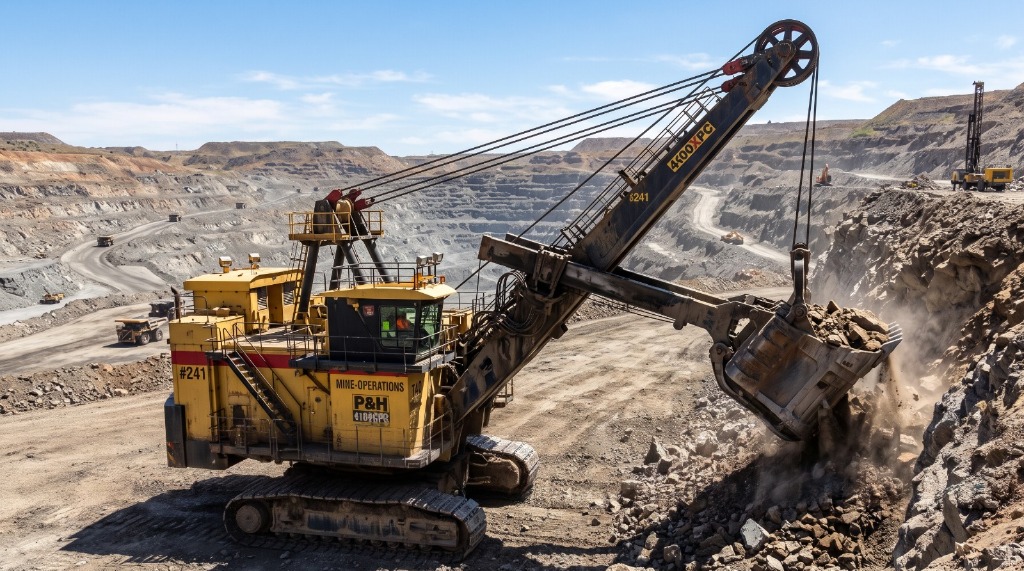
Rope shovels
Boom suspension ropes and dipper hoist rope.
Draglines
Hoist, drag and dump ropes for the bucket.
Mine hoists
Ropes for mine hoists and vertical winder systems.
Why leading surface mines partner with Bulker
Unmatched fatigue life
Our surface mining ropes are manufactured using high-density plastic compaction and optimized strand geometries, reducing internal friction and delivering up to 35% longer cycle life on draglines and electric shovels.
Severe abrasion resistance
Outer wire profiles specifically calculated to withstand abrasive drag over jagged pit floors, rock wall contact and harsh bench conditions without premature crown wear.
Reduced unplanned downtime
Bulker wire ropes undergo rigorous non-destructive magnetic testing and automated strand-tension balancing during manufacturing, virtually eliminating early operational strand failure.
Custom heavy spooling
Supplied in engineered lengths tailored to major shovel and dragline models, packaged on heavy-duty steel reels with protective wooden lagging for safe field deployment.
Precision manufacturing: how Bulker crafts ropes for extreme mining
Every Bulker wire rope is built in our state-of-the-art facility using proprietary metallurgical processes, continuous quality monitoring and zero-compromise tolerance checks.
01 Micro-purified carbon steel rods
We source exclusively high-carbon micro-alloyed steel rod stock with zero internal inclusions, giving our drawn wires extreme yield strength and resilience against micro-cracking under shock loads.
02 Controlled inline lead patenting
Prior to cold drawing, our steel wire undergoes thermal inline patenting to form a homogeneous fine-pearlite grain structure, essential for achieving high ductility alongside maximum tensile strength.
03 Precision rotary die compaction
Strands are passed through precision-calibrated rotary compaction rollers, flattening the outer wire crowns to maximize metallic area, smooth out surface contact and minimize friction.
04 Polymer infiltration & cushioning
During the closing phase, synthetic solid polymers are hot-extruded deep into the steel core, locking in factory lubrication while insulating internal strands against dynamic friction and moisture.
Zero-defect quality assurance guarantee
Every meter of Bulker surface mining rope undergoes continuous 360-degree high-definition laser diameter tracking, laser surface inspection and full-length electromagnetic flux (NDT) testing to verify 100% core and strand integrity before leaving our facility.
Advanced corrosion protection: Grade A galvanizing
Surface mining operations subject wire ropes to harsh atmospheric moisture, acidic runoff and slurry exposure. Bulker wire ropes feature a hot-dip Grade A heavy zinc coating applied in accordance with EN 10264-2 / ISO 2232 standards.
- Thick zinc barrier: provides a minimum zinc mass per unit surface area up to 3x thicker than standard commercial coatings, offering active sacrificial corrosion defence.
- High ductility bond: micro-alloyed zinc chemistry ensures the coating flexes smoothly around sheaves without flaking, cracking or peeling under intense dynamic bending.
- Extended service horizon: protects the underlying high-carbon steel wire against pitting corrosion, the primary catalyst for fatigue cracks in open-cast equipment.
Surface mining product lineup
| Code | Nominal diameter | Strand config | Application | Rope construction | Key characteristic |
|---|---|---|---|---|---|
| BWR-101 | 50 mm (2.0 in) | 8 strands (outer) | Electric shovel hoist | 8x55 compacted / plastic core | High bending fatigue life & plastic cushioning |
| BWR-102 | 54 mm (2.125 in) | 8 strands (outer) | Electric shovel crowd line | 8x36 compacted / cushion core | Crush resistant with smooth drum spooling |
| BWR-103 | 64 mm (2.5 in) | 6 strands (outer) | Medium dragline hoist | 6x36 Warrington Seale / Galv A | High tensile strength & corrosion barrier |
| BWR-104 | 70 mm (2.75 in) | 8 strands (outer) | Heavy shovel hoist / drag line | 8x36 compacted + plasticized | Extreme fatigue life under continuous shock load |
| BWR-105 | 77 mm (3.0 in) | 6 heavy strands | Heavy dragline drag rope | 6x19 outer heavy strand / Galv A | Maximum outer wire abrasion protection |
| BWR-106 | 95 mm (3.75 in) | 8 compacted strands | Ultra-class dragline drag rope | 8x36 compact strand / Grade A | Massive strength for high-capacity buckets |
| BWR-107 | 111 mm (4.375 in) | 8 structural strands | Extreme duty dragline main drag | Specialty 8-strand cushion core | Maximum core protection & severe wear life |
| BWR-108 | 38 mm (1.5 in) | 19 strands (2 layers) | Rotary blast-hole drilling rig | 19x7 rotation resistant / Galv A | Low-spin vertical stability under torque |
| BWR-109 | 44 mm (1.75 in) | 6 heavy strands | Haul road recovery towing line | 6x36 IWRC high-grade steel / Galv A | Superior shock absorption for heavy fleets |
Ready to optimize your surface mining fleet?
Speak with a Bulker technical sales engineer to select the ideal wire rope specification.
Technical brochure
Underground mining
Uncompromising reliability in deep-shaft operations.
Underground mining presents the harshest environments for wire ropes: extreme humidity, acidic run-off, severe multi-layer spooling wear and continuous dynamic cycles. BULKER WIRE ROPES engineered solutions are custom-built to maximize hoist availability, drive operational safety and dramatically lower cost-per-tonne extracted.
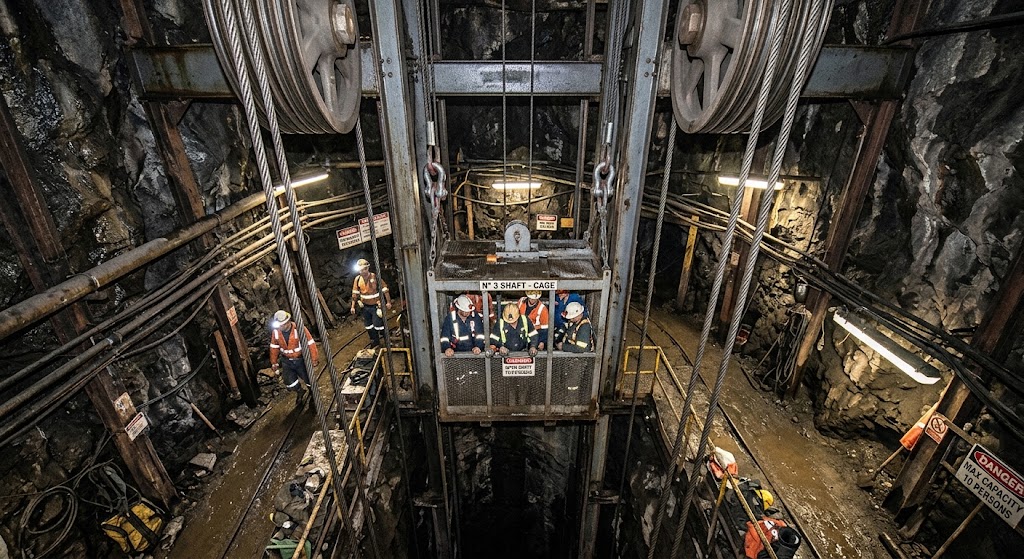
Why Tier-1 mining clients choose BULKER WIRE ROPES
Major underground mining operators globally standardize on Bulker products due to our commitment to structural longevity, structural integrity and custom manufacturing precision.
Dynamic fatigue resistance
Deep-shaft friction winders and drum hoists subject wire to relentless reverse bending cycles. Bulker's engineered plastic-impregnated cores and compacted strand geometries reduce internal friction by up to 60%, significantly extending bending fatigue life.
Superior crush & impact protection
Multi-layer drum spooling causes severe crushing forces on lower rope layers. Our specialized rotary strand swaging delivers a high fill factor (up to 76%), providing a smooth outer surface that resists cross-over crushing and drum scuffing.
Lowest total cost of ownership (TCO)
While initial purchase price is important, unplanned hoist downtime can cost thousands per hour. Bulker ropes deliver up to 2.5x longer service life compared to standard ropes, drastically cutting maintenance downtime and replacement frequency.
Complete batch traceability & testing
Every reel of Bulker wire rope comes with full EN 10204 3.1 certification, non-destructive electromagnetic inspection (NDT) reports and destructive sample testing to guarantee payload safety in man-riding shafts.
Underground application matrix
| Code | Application | Rope construction | Key advantage |
|---|---|---|---|
| BWR-301 | Koepe / friction hoists | 8-strand non-rotating compacted | High torque balance & wear resistance |
| BWR-302 | Double drum hoists | 6-strand plastic layered (EPIW) | Resists crushing in multi-layer spooling |
| BWR-303 | Slusher & LHD winches | 6×19 Seale metallic core | Maximum abrasion resistance against rock |
| BWR-304 | Guide & balance ropes | Half-locked / full-locked coil | Smooth surface, minimal vibration & sway |
Engineered protection: Grade A galvanizing technology
Underground mines feature damp, acidic air, saline groundwater and harsh chemical slurry. Standard commercial zinc coatings deteriorate rapidly, leading to undetected micro-pitting and accelerated strand failure. Bulker Wire Ropes uses specialized Grade A hot-dip galvanizing across all mining series.
Heavy coating mass (ISO 2232 / EN 10264-2)
Our Grade A galvanizing applies a dense, uniform zinc layer exceeding 260 g/m² (for standard diameters), which is double the zinc weight of standard commercial ropes (Grade B). This creates a thick sacrificial barrier against corrosive mine water.
Micro-alloyed zinc bond
Through an advanced inline bath process with micro-alloyed elements (zinc-aluminium / rare earth additives), the zinc layer achieves superior mechanical bonding with the high-carbon steel substrate, preventing flaking during sharp bends.
Benefits of Grade A galvanize in underground mine shafts
- Elimination of internal hydrogen embrittlement: specially controlled acid pickling and thermal annealing during galvanizing prevents micro-cracking under high tension.
- Synergistic protection with synthetic lubricants: Grade A zinc works in tandem with Bulker's factory-injected pressure lubricants, trapping the protective zinc layer and shielding internal wires from moisture ingress.
- Smooth surface for electromagnetic testing (NDT): uniform coating thickness prevents false readings during routine shaft safety magnetic flux leakage inspections.
Featured underground product codes
BWR-301
Deep-shaft friction hoist rope
8×26 Warrington Seale + plastic coated core
- Compact strands for max sheave contact
- High torque stability under extreme suspension
- Grade A heavy galvanized finish
BWR-302
Heavy drum shaft hoist rope
6×36 Warrington Seale + solid plastic core
- Extremely high crushing resistance on drum
- Polymer cushioning prevents strand friction
- Ideal for multi-layer fleet angling
BWR-303
Heavy duty slusher & drag rope
6×19 Seale + independent wire rope core (IWRC)
- Thick outer wires for extreme rock abrasion
- Grade A zinc shields against mine floor mud
- High impact shock resistance
BWR-304
Locked coil guide rope
Full-locked Z-shape outer wires
- Interlocked profile keeps smooth surface
- Minimizes wear on conveyance slippers
- Maximum corrosion resistance in shaft drafts
Ready to upgrade your underground shaft reliability?
Contact our underground engineering specialists for custom reel lengths, end terminations and site audit services.
Technical product guide
Bucket wheel excavator wire ropes
Engineered for continuous high-tonnage mining, high cyclic fatigue and severe abrasive environments.
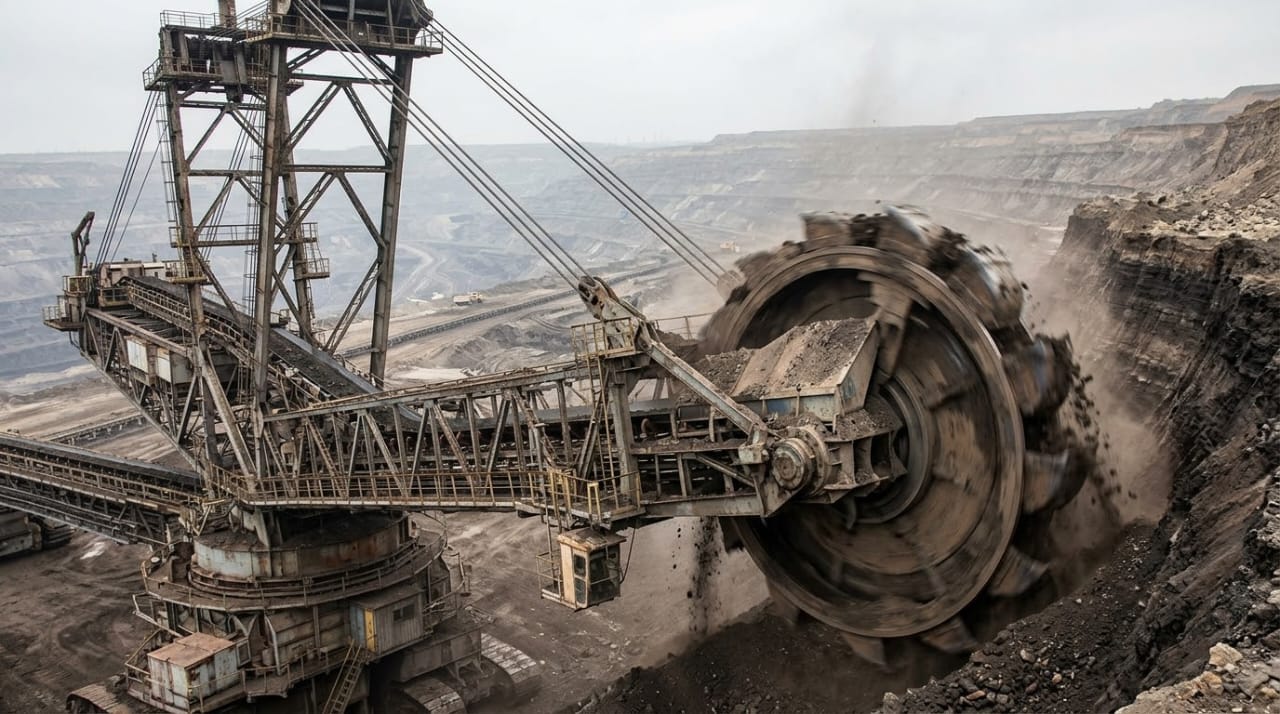
Bucket wheel excavators (BWE) represent the pinnacle of continuous surface mining equipment. Downtime on a primary excavator halts the entire material transport chain. Mining conglomerates globally rely on Bulker Wire Ropes because our engineering directly eliminates premature structural failure, wear fatigue and unexpected rope replacement cycles.
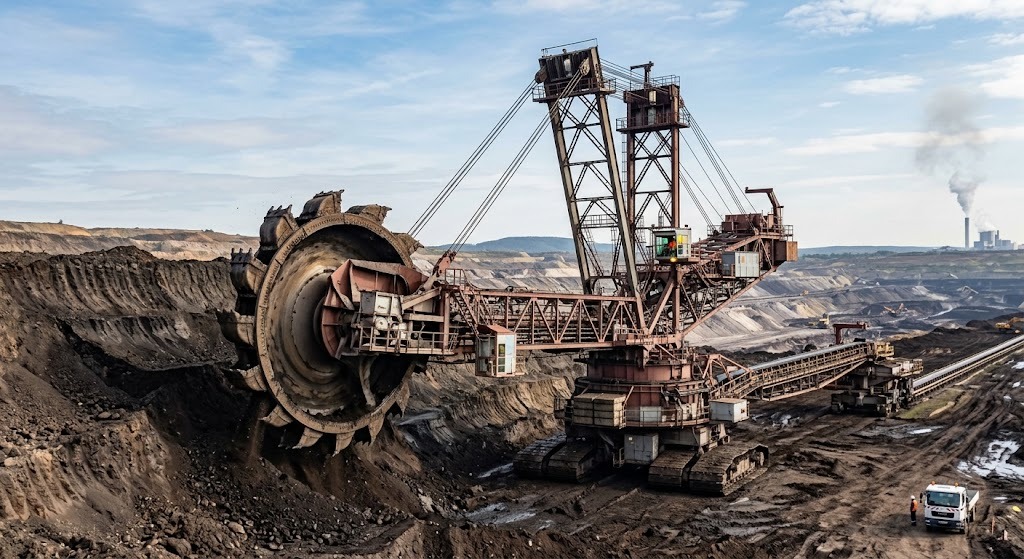
Multi-strand ropes
Bucket-wheel excavators (BWE)
Mechanical architecture of rope-luffed BWEs
Unlike hydraulic excavators reliant on heavy cylinders, this system uses high-strength multi-strand steel wire ropes to control the vertical movement of the wheel boom. Ropes travel from the winch system, route over the mast sheaves and connect to the wheel boom tip.
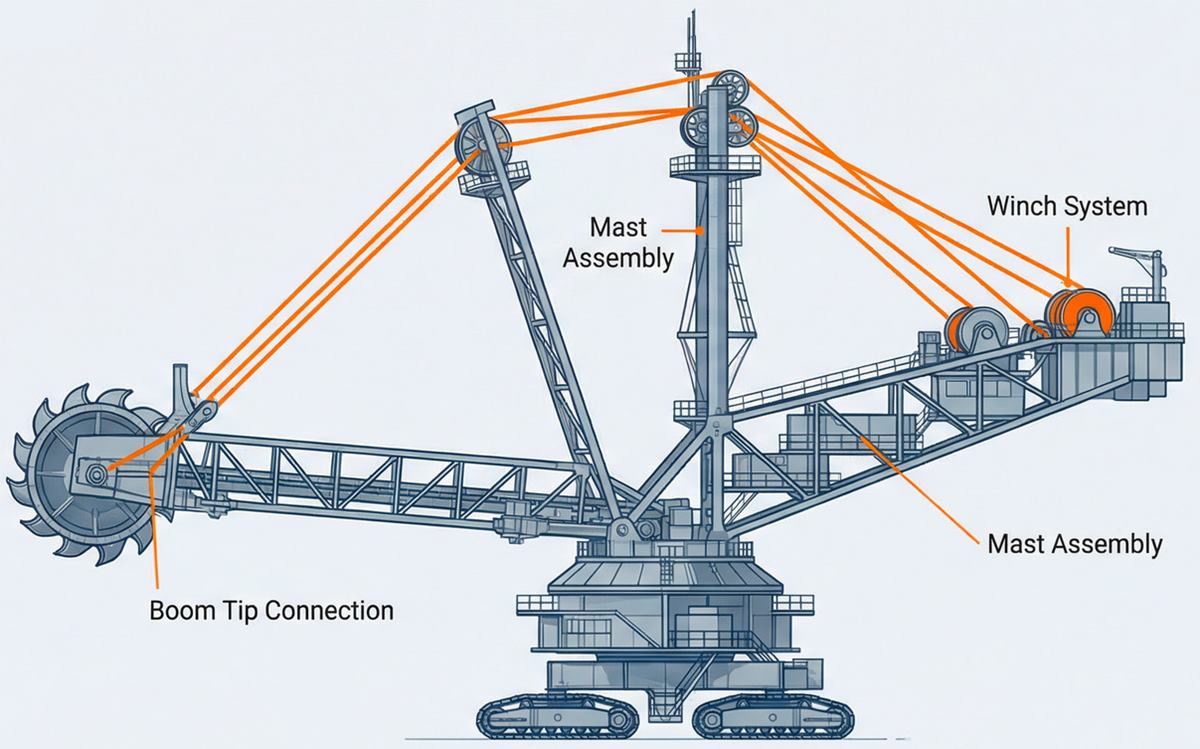
Winch & drive configuration
Large electric winches on the superstructure or within the counterweight boom drive the lifting motion through precision control.
Stability & dynamic equilibrium
Wire ropes reduce front deadweight, shifting the centre of gravity closer to the rotation axis; the counterweight boom balances the wheel boom through tension.
Shock absorption
The inherent elasticity of steel wire ropes damps high-impact shock loads and vibrations.
Longer booms
The rope system supports longer boom designs, increasing excavation block height and width and reducing crawler repositioning.
Inspection & safety
Scheduled inspections (broken wires, corrosion, diameter loss, lubrication), magnetic flux leakage (MFL) testing, tension equalization across parallel ropes and redundant hoist brakes.
Proven ROI in continuous open-cast operations
Why operators choose Bulker Wire Ropes
01 Maximized fatigue life
Specialized plastic-infilled core designs absorb dynamic shock loads and prevent internal strand-to-strand friction under heavy bending cycles.
02 Superior abrasion shield
Compacted outer strands present a flattened outer profile, distributing sheave wear over a 40% larger surface area than conventional wire ropes.
03 Grade A galvanic protection
100% heavy zinc coating ensures total resistance against acidic pit waters, aggressive humidity and atmospheric oxidation.
04 Precise diameter stability
Tight manufacturing tolerances minimize fleet angle wear and prevent crushing on multi-layer winch drums during luffing manoeuvres.
Application mapping on BWE systems
Boom hoist / luffing
Requires high fatigue resistance and high breaking force to safely elevate massive bucket wheel booms under varying material loads.
Discharge boom hoist
Demands superior spooling behaviour on smooth and grooved winch drums with zero rotation tendencies under severe dynamic load shocks.
Counterweight tensioning
High structural stability and ultimate resistance against atmospheric corrosion in static/semi-static tension ropes.
Rope integration: BWR-800 series on the main boom hoist, BWR-600 series on the discharge boom and tension ropes.
High-performance BWE wire rope matrix
Technical specifications & product codes
All Bulker wire ropes engineered for BWE applications are designated under the BWR series code system. Below are standard diameters, strand configurations and minimum breaking forces (MBF) calibrated for high-capacity excavators.
| Code | Nominal dia. | Strand construction | Core type | Finish grade | Min. breaking force | Unit weight |
|---|---|---|---|---|---|---|
| BWR-612 | 28 mm | 6x36 Warrington Seale | EPIW (plastic infilled) | Grade A galvanized | 582 kN | 3.35 kg/m |
| BWR-618 | 32 mm | 6x36 Warrington Seale | EPIW (plastic infilled) | Grade A galvanized | 760 kN | 4.38 kg/m |
| BWR-625 | 38 mm | 6x41 Filler Wire compacted | IWRC (steel core) | Grade A galvanized | 1,080 kN | 6.18 kg/m |
| BWR-810 | 42 mm | 8x26 compacted outer strands | EPIW (plastic infilled) | Grade A galvanized | 1,340 kN | 7.55 kg/m |
| BWR-812 | 48 mm | 8x36 compacted outer strands | IWRC (steel core) | Grade A galvanized | 1,750 kN | 9.82 kg/m |
| BWR-820 | 54 mm | 8x36 swaged heavy duty | EPIW (plastic infilled) | Grade A galvanized | 2,210 kN | 12.45 kg/m |
| BWR-835 | 60 mm | 8x41 compacted high-strength | EPIW (plastic infilled) | Grade A galvanized | 2,730 kN | 15.30 kg/m |
| BWR-900 | 64 mm | 8x47 extra high tensile | Full synthetic core shield | Grade A galvanized | 3,110 kN | 17.40 kg/m |
Bulker Grade A galvanizing technology (EN 10264-2 Class A compliant)
Standard commercial wire ropes feature thin zinc coatings that quickly degrade when subjected to abrasive coal/ore dust and acidic runoff water. Bulker Wire Ropes uses a proprietary Grade A heavy hot-dip galvanization process.
Maximum coating thickness
Zinc mass ranges between 230 g/m² and 290 g/m² depending on wire gauge, offering up to 3x longer corrosion resistance compared to Class B coatings.
High-adhesion zinc bond
Advanced micro-alloying prevents zinc flaking or cracking during high-stress wire compaction and tight bending over sheave grooves.
Strand & core construction spotlight
Compacted outer strands (BWR-800 series)
Individual outer strands are drawn through precision shaping dies to flatten outer crown wires. This reduces localized sheave pressure, improves drum spooling geometry and dramatically lowers internal friction.
EPIW (encapsulated plastic inner wrapper)
A solid polymer layer injected between the steel core and outer strands seals in factory lubricant while permanently excluding abrasive dirt, moisture and fine ore slurry.
Need custom construction matching specific OEM winch drum profiles?
Contact the Bulker engineering team.
Technical product sheet
Shore-to-barge transfer systems
Heavy-duty marine solutions.
High-throughput shore-to-barge loading demands exceptional fatigue resistance, continuous shock-load absorption and rigorous marine corrosion protection. BULKER WIRE ROPES engineers specialized steel wire ropes built for continuous duty in harsh marine environments, reducing downtime and lowering total operating cost.
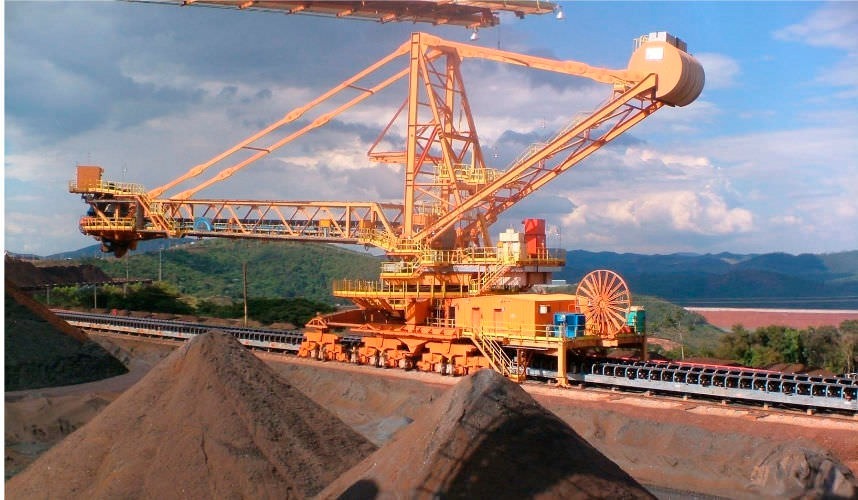
High-tensile ropes
Shore-to-barge positioning
Mechanics of shore-to-barge cable positioning
Shore-based mobile mining machines (often modified excavators or dozers) or stationary winch stations use high-tensile wire ropes to anchor and manoeuvre floating mining barges. The ropes act as positioning tools: by triangulating the barge's location, operators achieve controlled movement without onboard propulsion, which is prone to failure in sludge or debris-filled waters.
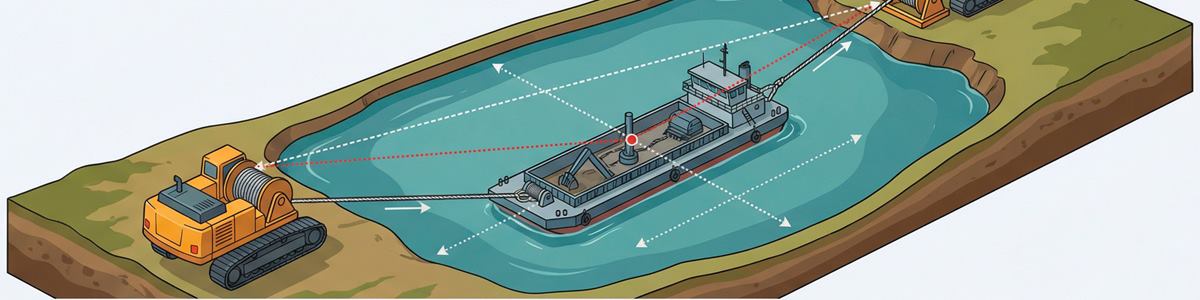
Dynamic tension control
Shore machines adjust cable tension continuously to counteract wind, water currents and dredging or pumping forces.
Systematic sector sweeping
Coordination between shore machines and barge enables sequential processing of specific sectors.
High-torque viscosity management
In oil sands and aggregate mining, land-based machines provide the torque to drag the barge through media that would stall conventional propellers.
Metallurgical integrity
Ropes constructed to withstand cyclic loading, abrasive wear from grit and corrosion in acidic mining waters.
Snap-back prevention
Continuous monitoring of cable tension and fleet angles to prevent rope failure and snap-back.
Shore-to-barge product range
BWR-445
44 mm standard marine
- Strand count
- 5 strands
- Core
- Independent wire rope core (IWRC)
- Primary size
- 44 mm
- All diameters
- 28, 32, 36, 38, 40, 42, 44, 46 mm
- Application
- Shore loading and winching, boom hoists and barge positioners.
BWR-546
54 mm heavy duty
- Strand count
- 6 strands
- Core
- Full steel structural core
- Primary size
- 54 mm
- All diameters
- 48, 50, 52, 54, 56, 58 mm
- Application
- High-speed bulk loader hoists, heavy luffing systems, offshore transfer.
BWR-606 New
60 mm flagship heavy
- Strand count
- 6 strands
- Core
- Reinforced high-tension IWRC
- Primary size
- 60 mm
- All diameters
- 60, 62, 64, 68, 72 mm
- Application
- Ultra-heavy capacity shore loaders, extreme wave-action environments.
Technical specifications & diameter matrix
| Product code | Primary size | Strand config. | All available diameters (mm) | Coating grade | Breaking load (primary size) | Primary usage |
|---|---|---|---|---|---|---|
| BWR-445 | 44 mm | 5 strands | 28, 32, 36, 38, 40, 42, 44, 46 | Class A heavy galv. | 1,280 kN | Shore loading and winching |
| BWR-546 | 54 mm | 6 strands | 48, 50, 52, 54, 56, 58 | Class A heavy galv. | 1,940 kN | Heavy bulk material handling |
| BWR-606 New | 60 mm | 6 strands | 60, 62, 64, 68, 72 | Class A heavy galv. | 2,410 kN | Ultra-capacity marine loading |
Maximum zinc mass coating for saltwater endurance
Superior corrosion protection: Grade A galvanizing
All BULKER shore-to-barge wire ropes are manufactured exclusively using heavy Grade A hot-dip galvanization compliant with ISO 2232 / EN 10264-2 requirements. By applying a high-density, pure zinc layer thoroughly bonded to each individual wire, our ropes provide up to 2.5x longer service life against saltwater spray, atmospheric humidity and splash-zone oxidation compared to standard commercial coatings.
Why industry leaders choose BULKER WIRE ROPES
- Engineered for dynamic fatigue resistance: purpose-built lay geometry ensures smooth spooling on multi-layer drums and reduces bending stress over sheaves during constant wave-action movement.
- Proven total cost reduction: higher fatigue life and the Grade A anti-corrosion layer dramatically decrease rope replacement frequency and unscheduled berth downtime.
- Full traceability & certification: every reel of BWR rope ships with 100% material test certificates, mill inspection [TO PROVIDE: end of the sentence, cut off in the PDF].